

How to Ensure Traceability of Welding Procedure Records?
- Blog
- How to Ensure Traceability of Welding Procedure Records?
How to Ensure Traceability of Welding Procedure Records?
Table of Contents
- Why Traceability Matters in Welding Records
- Structure of a Welding Procedure Record
- Linking to Material Certificates
- Welder Qualification Records
- Weld Identification System
- Parameter Records and Deviations
- Linking Inspection Results to Welds
- Revision and Record Control
- Digital Records and Archiving
- Conclusion
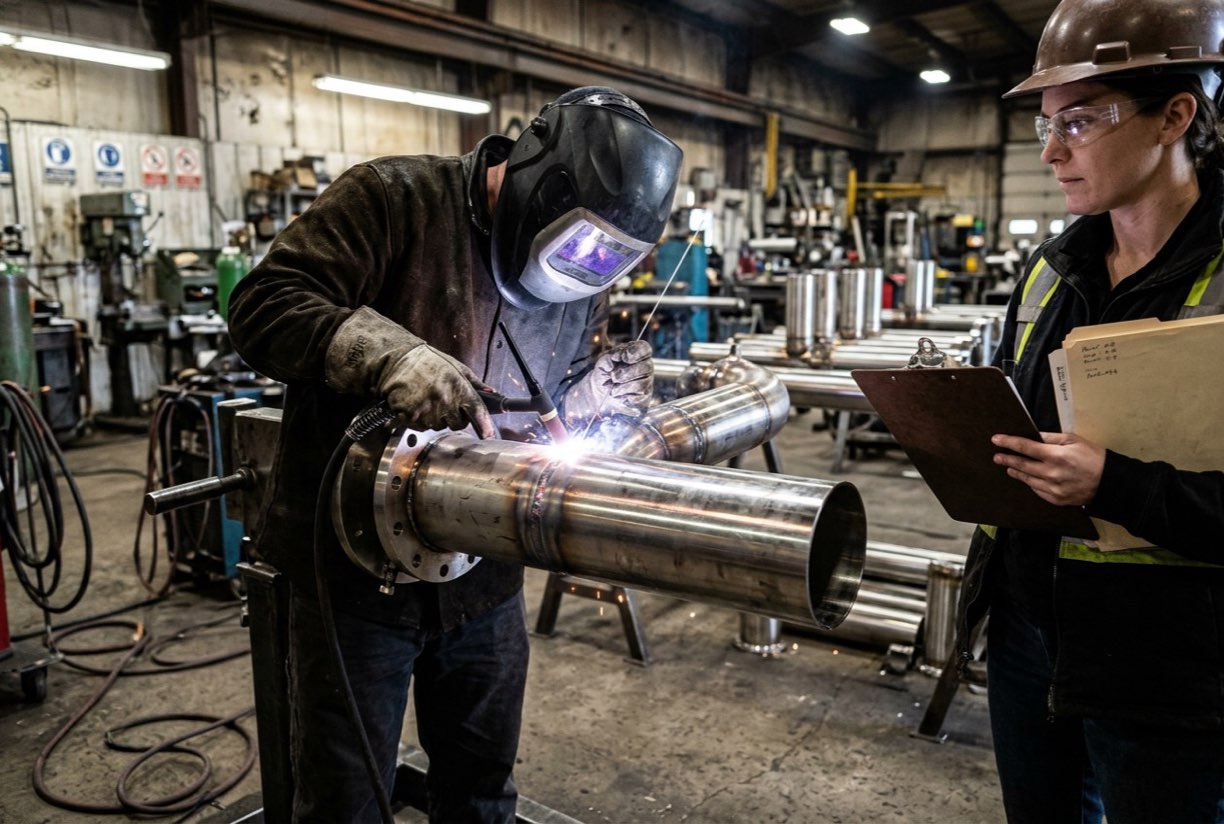
The reliability of a welded piece of equipment depends not only on how the weld was made but also on whether that can be proven later. Traceability means being able to show, looking back from today, which material, which welder, which procedure and which parameters produced a given weld.
Why Traceability Matters in Welding Records
When a welding defect appears, the record must be complete in order to find its cause. If it cannot be determined which welder worked with which parameters, the extent of the problem cannot be determined either. This can require a wide inspection or the reproduction of the whole item.
A traceable record is also the basis of the acceptance and handover process. It must be shown by evidence that the design and contract requirements have been met.
Structure of a Welding Procedure Record
A welding procedure record covers the welding process, the material and thickness range, the filler material, preheat, interpass temperature, shielding gas and current and voltage parameters. The record should also show which standard the procedure was prepared to and the approval date.
The procedure number and revision should be stated clearly on every welding record. If the revision applied is unclear, traceability is weakened.
Linking to Material Certificates
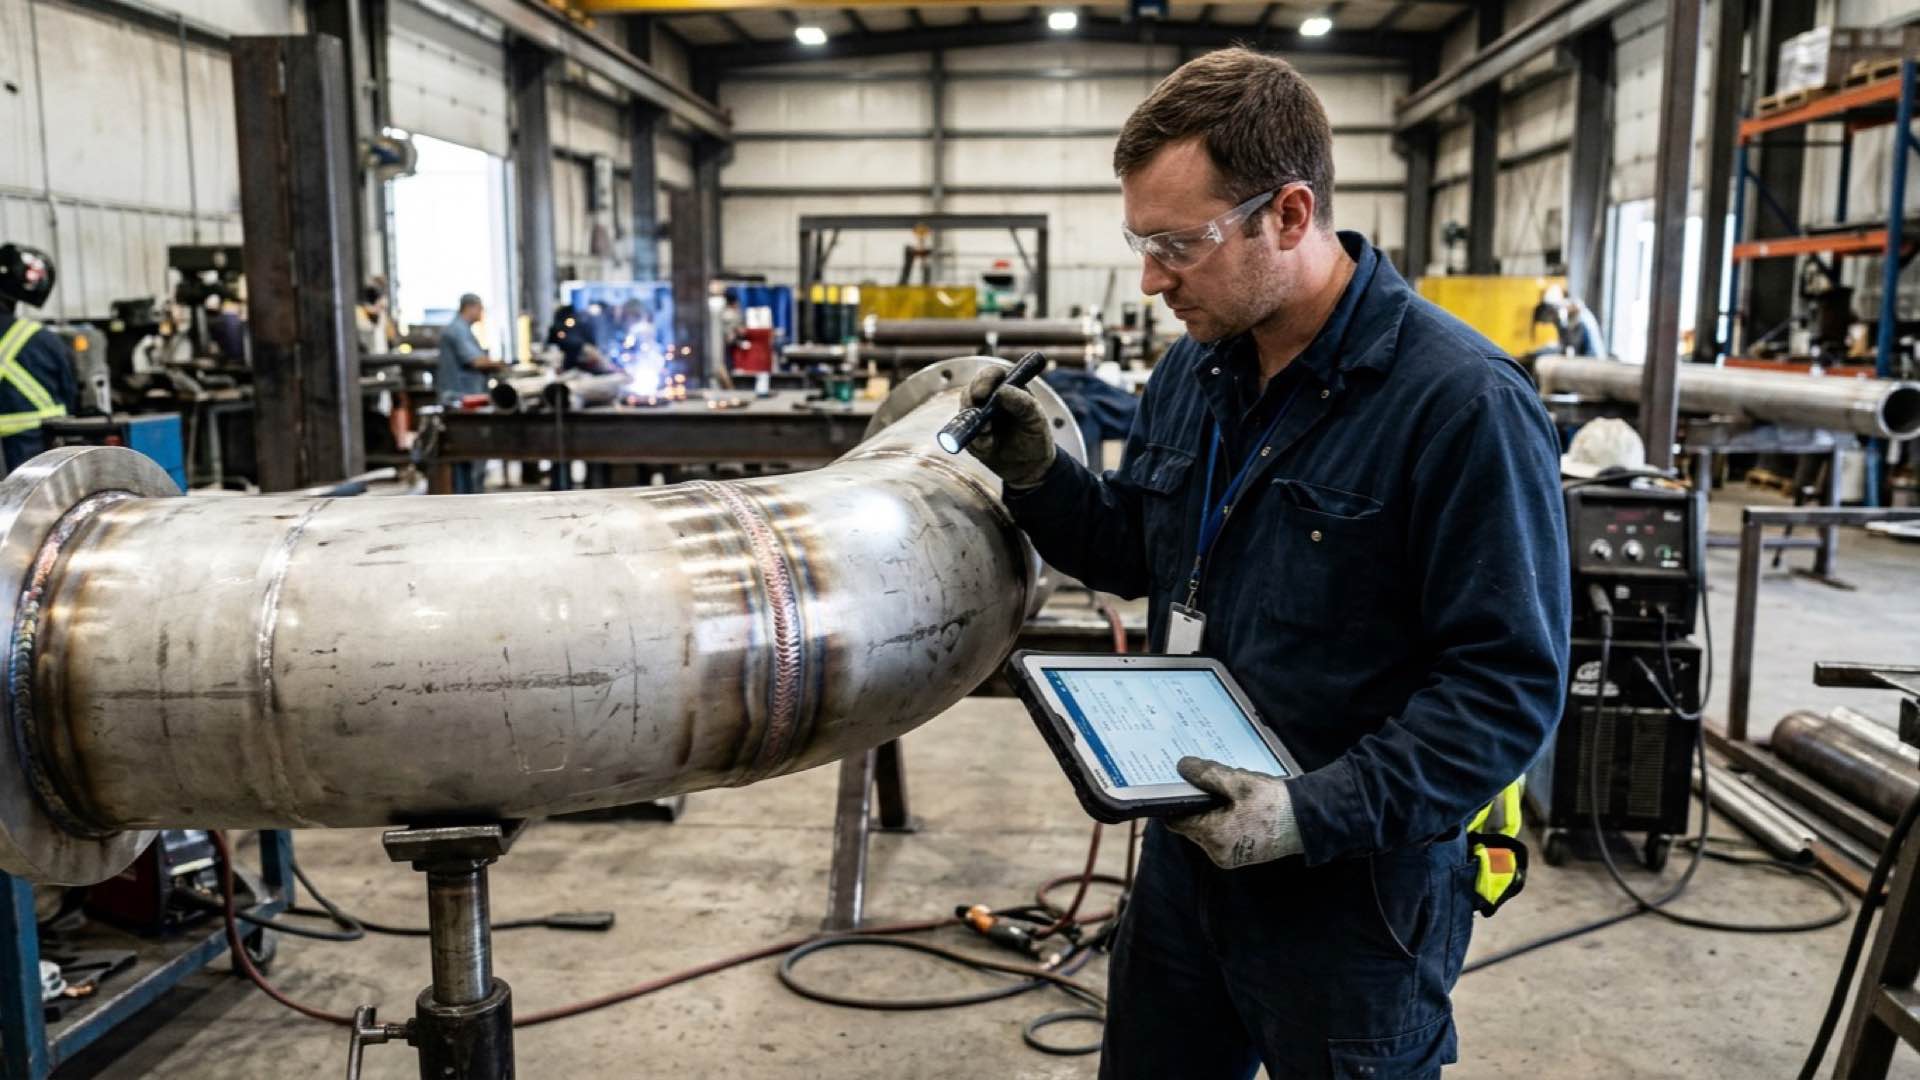
The certificate of the base material and of the filler material used in each weld should be linkable to that weld. The heat number or batch number of the material should appear in the welding record. This link allows the origin of the material to be verified later.
A part whose material certificate is missing or whose record was not made is considered weak in terms of traceability.
Welder Qualification Records
A welder's qualification certificate shows which process, position and material it is valid for. Every weld record should include the welder identity and the relevant qualification information. The validity period of the qualification should also be checked.
The link between the welder's record and the weld is one of the pieces of information most needed when analysing a fault.
Weld Identification System
Giving every weld a unique identity is the cornerstone of traceability. A weld identity can include the equipment number, the joint type and a sequence number. The identity system should be used the same way on the drawing and in the records.
The identity should be fixed before welding and recorded. An identity given afterwards reduces the reliability of the record.
Parameter Records and Deviations
The recorded welding parameters should be compared with the range in the procedure. If a parameter goes outside the range, the deviation should be recorded. The deviation should be handled by assessing its effect on the quality of the weld.
Parameter recording should be done automatically where possible rather than written by hand. Manual records carry the risk of misreading and late entry.
Linking Inspection Results to Welds
The result of every check, whether visual inspection, radiography, penetrant testing or another method, should be linked to the relevant weld identity. This makes it traceable which weld passed which inspection and which weld was repaired.
Repair records should be kept as separate records rather than written over the original record. The reason for the repair, the work done and the result of the next inspection should be added.
Revision and Record Control
When the welding procedure is revised, it should be assessed under what conditions welds made to the old revision can be accepted. The revision information on the records should agree with the procedure applied.
Regular record control helps catch missing fields and inconsistencies early. The check should be carried out by having someone other than the author review the record.
Digital Records and Archiving
Digital record systems make searching, matching and archiving easier. However, data integrity, access rights and backup rules must also be defined for digital records. A record that can be altered weakens traceability.
The archive period should be set according to the project contract and the applicable regulations. Records should remain accessible for the life of the equipment.
Conclusion
Traceability in welding procedure records is achieved through the procedure, material certificates, welder qualification, weld identity, parameter records, inspection links and revision control. When these links are firmly in place, the history of any weld can always be shown with evidence.
SS Proje supports the creation and management of quality records in welded fabrication. The record format, acceptance criteria and archive period should be set for each project according to the standard and the project specification.